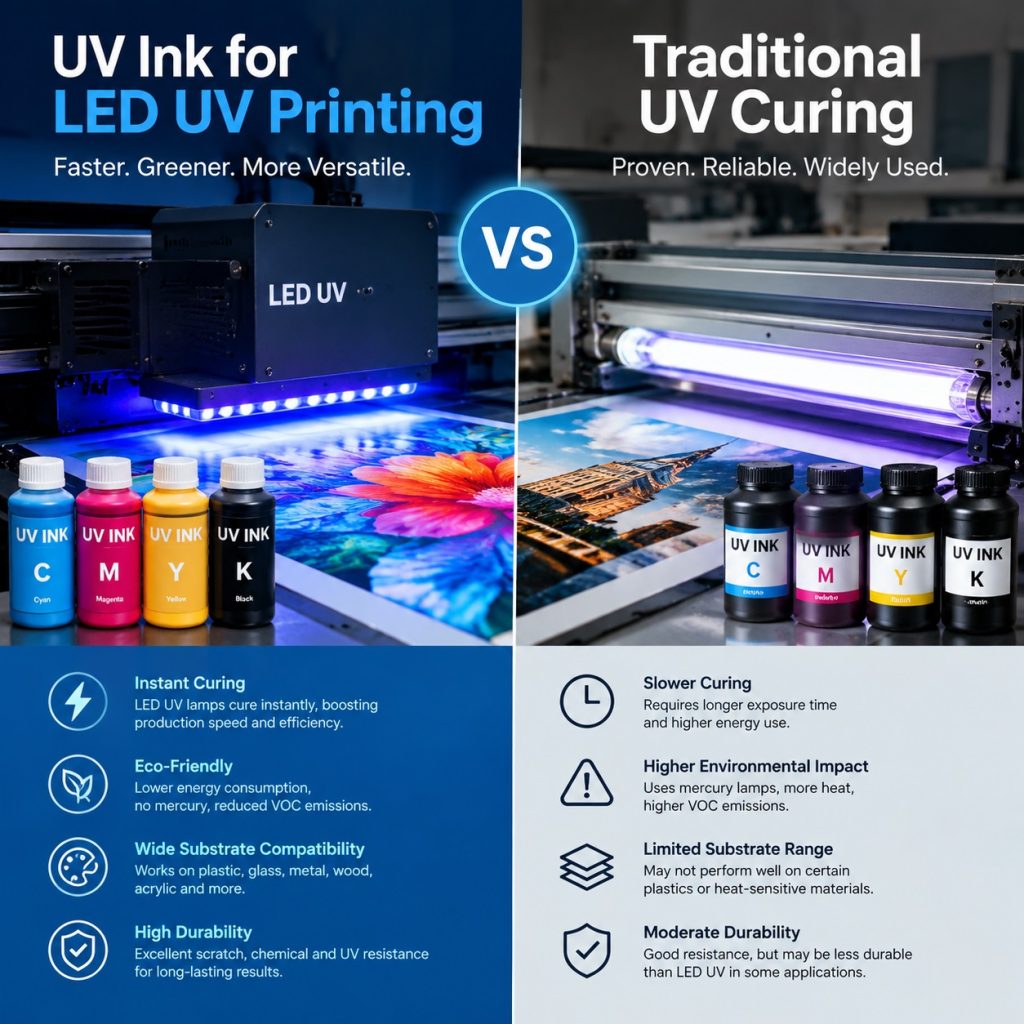
UV Ink for LED UV Printing vs. Traditional UV Curing: What Buyers Should Know


Buying UV InkThe curing lamp is not a lightbulb you swap like a burnt-out bulb. It is a chemical reactor, a speed limiter, and a hidden line item in your cost per print. That is why the choice between LED UV printing and traditional UV curing starts with the ink, not the lamp.

A UV ink is a package: oligomers, monomers, pigments, additives, and photoinitiators. The photoinitiators are the part that wake up when light hits them. Change the light source, and you change which photoinitiators actually work. LED UV curing usually fires around a narrow band, often 385 nm or 395 nm. Traditional UV curing from mercury or metal halide lamps throws a broad spectrum, from deep UV into visible light, plus a lot of infrared heat. Same word, UV, very different dinner invitation for the chemistry.

That difference matters before you sign a purchase order.

LED UV printing has obvious curb appeal. Lamps are instant on and instant off, so you are not waiting for warm-up or letting a bulb idle. They run cooler, which helps with thin films, heat-sensitive substrates, and some packaging stocks. They last far longer than mercury bulbs, and they avoid the ozone and mercury disposal headaches that come with traditional UV. For a shop trying to cut energy costs and simplify maintenance, that is a strong pitch.

But the ink has to match the lamp. LED UV inks are formulated with photoinitiators tuned to the LED wavelength. Put a traditional UV ink under an LED lamp, and you may get a sticky surface, poor through-cure, or adhesion that fails after a fold or a tape test. Put an LED ink under a traditional mercury lamp, and you may over-cure or waste chemistry. Some inks are hybrid and can run under both, but hybrids are a compromise, not a magic bullet.

Traditional UV curing still owns several corners of the market. Mercury lamps deliver high peak intensity and a broad spectrum, which can be an advantage for thick ink films, highly pigmented whites, dark blacks, and high-speed production where every millisecond counts. The broad spectrum can also reach deeper into the film and handle formulations that LED wavelengths struggle to cure. If your work is heavy coverage, high opacity, or unusual specialty coatings, traditional UV may still be the safer production horse.

The buyer’s first question is not “Which is newer?” It is “What am I printing, on what, at what speed, and with what performance requirement?” A narrow-web label printer running heat-sensitive film at moderate speed may find LED UV a clear win. A wide-format shop laying down thick white on rigid boards at high speed may find traditional UV more forgiving. A packaging printer with food-contact concerns needs to look beyond curing speed and examine migration, low-migration ink systems, and whether the chosen chemistry is approved for the application.

Then there is the money. LED UV often wins on electricity, lamp life, and maintenance. Traditional UV often wins on ink cost per kilo and the sheer maturity of the supply chain. But the real number is total cost per sellable print. Add up energy, bulb replacement, reflector cleaning, ozone extraction, chillers, downtime, scrap rate, and the labor spent chasing adhesion problems. A cheaper ink that forces you to slow the press or reject more jobs is not cheaper. A higher-priced LED ink that lets you run cooler, faster, and with fewer lamp changes can pay for itself in a few months.

Do not let a sales sheet decide this for you. Ask for a cure test on your substrate, with your artwork, at your target speed. Check surface cure with a thumb twist or MEK rub. Check through-cure with a cross-hatch adhesion test, a fold, a crease, and a tape pull. If the application demands it, ask for migration data and regulatory documentation. Run the same test under both lamp technologies if you can. The ink that looks best in a brochure may not be the one that survives a real shift.

Also look at the press environment. LED UV modules are smaller and cooler, which can open up machine design options. Traditional UV lamps need warm-up, shutters, exhaust, and more heat management. That extra hardware costs space and service time. If you already have a traditional UV line that is running well, switching to LED may mean new ink, new lamp modules, new maintenance routines, and a learning curve. The upgrade is not just a bulb swap. It is a system change.

For buyers, the smart move is to separate the lamp from the ink, then reunite them in a trial. Tell your ink supplier what lamp, what wavelength, what speed, and what substrate. Tell your lamp supplier what ink chemistry you plan to run. Make them talk to each other. The shops that get this right treat UV curing as a partnership between chemistry and light, not as a battle between old and new.

If you are specifying a new press, ask for a side-by-side cure trial before the invoice. If you are switching an existing line, ask for a migration and adhesion plan, not just a price per kilogram. If you are a brand owner approving packaging, ask your converter which ink and curing system will be used, and whether the cure window is robust enough for the full run. Those questions protect the print, the schedule, and the bottom line.

LED UV is not automatically better. Traditional UV is not automatically obsolete. The right choice is the ink and curing combination that cures completely, adheres reliably, meets the regulatory bar, and hits your cost target on the substrates you actually run. Everything else is just lamp talk.
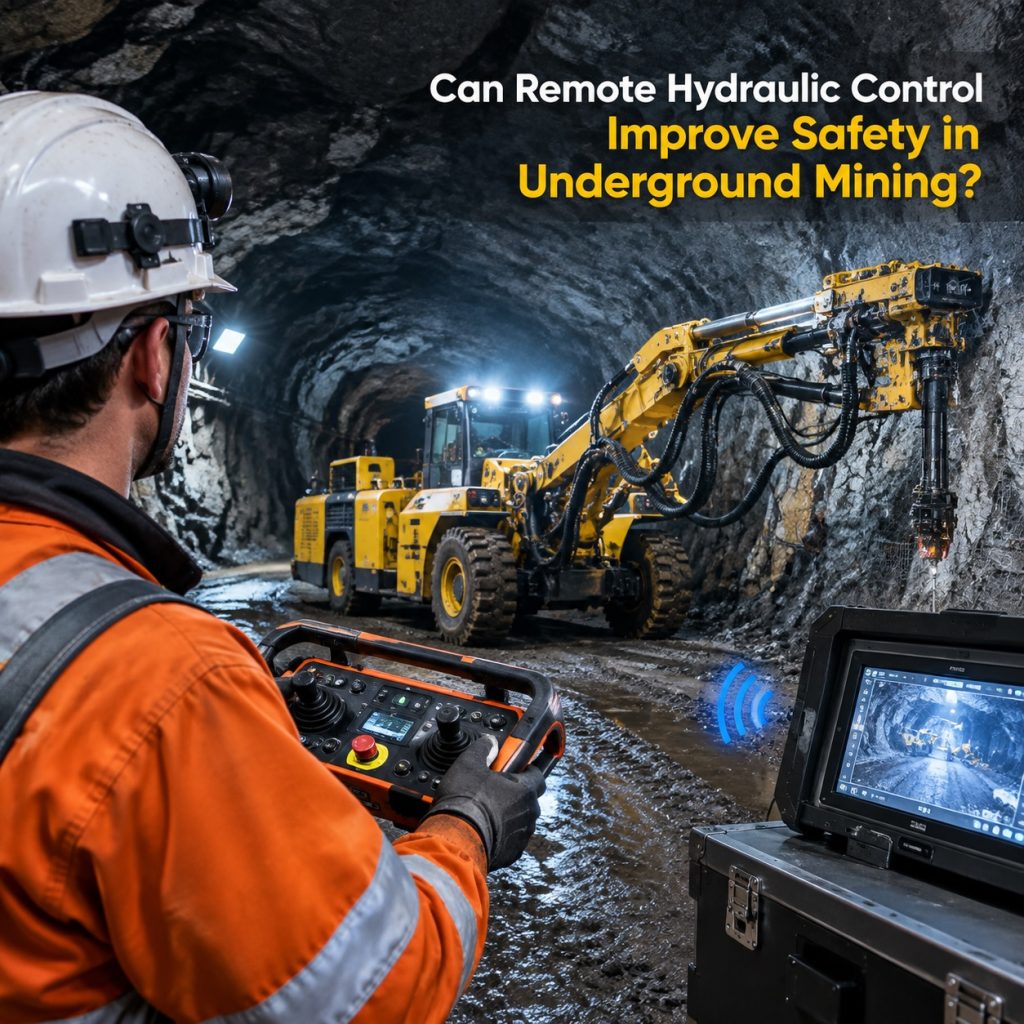
Can Remote Hydraulic Control Improve Safety in Underground Mining?


Hydraulic Control System Ask a roof bolter operator what worries them most and you won’t hear about cycle times. You’ll hear about the two metres of unsupported ground overhead, the sound of a joint opening somewhere above the canopy, and the fact that their hands are on a hydraulic control bank that sits directly underneath it.

That is the uncomfortable arithmetic of underground mining. The person best placed to operate the machine is often the person most exposed to the hazard the machine is supposed to manage. Remote hydraulic control attacks that arithmetic directly, and it is worth understanding why it works, where it fails, and what it actually changes on a shift.

Start with the geography of risk. On a development heading, the operator of a bolter or a jumbo sits or stands within a few metres of an unsupported back, a working face that has not yet been scaled, and a boom that swings several tonnes of steel through a space barely wide enough to contain it. On a longwall, the shield advance is controlled from a position that is technically protected but still within the dust and noise envelope of the face. In a load-haul-dump cycle, the operator is in the path of the machine they are driving, especially in poor visibility or around drawpoints.

Remote hydraulic control moves the human out of that envelope. Instead of a manual lever bank plumbed directly into the valve stack, the machine carries electro-hydraulic actuators, proportional solenoids or piloted directional valves that respond to electrical commands. Those commands come from a joystick console, a radio pendant, or a teleremote station in a safe location, usually in supported ground with a clear line of sight or a camera view of the working area.

The safety case is not theoretical. Take the bolter operator standing thirty metres back in supported ground with a radio pendant and a deadman trigger. If the back starts to move, they are not under it. If a hose fails and sprays hot oil at two hundred bar, they are not in the spray path. If the boom swings unexpectedly, they are not between it and the rib. Dust, diesel particulate, noise and whole-body vibration all drop, because the operator is no longer sitting in the worst of it for ten hours a shift. Cumulative exposure is a safety issue even when no single event hurts anyone.

The gains get more interesting when you add feedback. A modern remote system is not just a long cable. Pressure transducers on the valve blocks, position sensors on the cylinders and a controller that knows the machine’s state mean the operator can see what the hydraulics are doing rather than guessing from sound and feel. Fault codes tell a fitter which valve is sticking before it strands a machine in a decline. Diagnostics that used to take two hours of crawling over a machine in a hot heading become a fifteen minute job at a laptop in a crib room. Every hour removed from that environment is an hour of exposure eliminated.

There is a genuine productivity argument too, and it is not just marketing gloss. A bolter that can be repositioned remotely, or a LHD that can be operated from a station outside the muckpile, keeps running through conditions that would normally stop the job. Rockfall risk, poor ventilation, heat or a face that is simply too dangerous to stand under no longer automatically mean downtime. Remote operation lets work continue from a position of safety, which is the version of safety that actually gets adopted on site. If the safe method is slower and more painful, crews will find a way around it. If it is faster, it sticks.

Now the honest part. Remote hydraulic control does not remove the hazard, it relocates the operator and, in some cases, the hazard. Line of sight teleremote is not the same as being there. Depth perception on a camera feed is poor, and a machine that cannot see a person behind it is a crushing risk. Latency matters more than vendors like to admit; a two hundred millisecond delay on a boom function feels like driving on ice. Radio links drop out in curves and around pillars, which is why failsafe behaviour has to be designed in from the start, not bolted on. Loss of signal should stop the machine, hold the load, and default to a safe state, every time.

Hydraulics themselves remain hydraulics. Hoses still burst, filters still clog, oil still gets hot, and someone still has to service all of it. Remote control reduces the number of people in the red zone during operation, but maintenance still requires hands on the machine. The real safety gain comes from reducing the frequency and duration of that exposure, not from pretending it disappears.

There is also a human factors trap. Operators who are physically removed from a machine can become less attentive to what it is doing. The seat-of-the-pants feedback that warns an experienced operator that something is wrong disappears. Good systems compensate with alarms, interlocks and haptic or visual cues. Bad systems just hand someone a joystick and a camera and hope for the best.

So does remote hydraulic control improve safety? Yes, meaningfully, when it is specified properly and matched to the task. The strongest results come from three things being true at once: the operator is genuinely outside the hazard envelope, the control system fails safe on loss of communication, and the machine gives the operator enough feedback to make good decisions. Get those right and you are removing people from unsupported ground, from hot oil, from noise and dust, and from the path of heavy equipment that does not stop for anyone.

Get them wrong and you have spent a lot of money moving a problem thirty metres away. That distinction is worth more attention than any specification sheet, and it is the one that decides whether the investment pays back in incident reports avoided or just in a slightly quieter cab.

Copyright ©2026 . All Rights Reserved | Diy Tips On Business